Test & V&V
Test limits with Cp and Cpk
Limits nobody has reviewed become either false alarms or free riders. Cp and Cpk per step show which.
How you work it in Colleag
- 1
Ask for process capability per test step.
- 2
The colleague computes Cp and Cpk from test data.
- 3
Negative Cpk and overly wide limits are flagged.
- 4
Adjust the limits with the evidence saved.
A worked example
“Which test steps in the X200 final test have negative Cpk?”
The steps sorted by Cpk, with measurement distributions against the limits and suggestions for which limits to review.
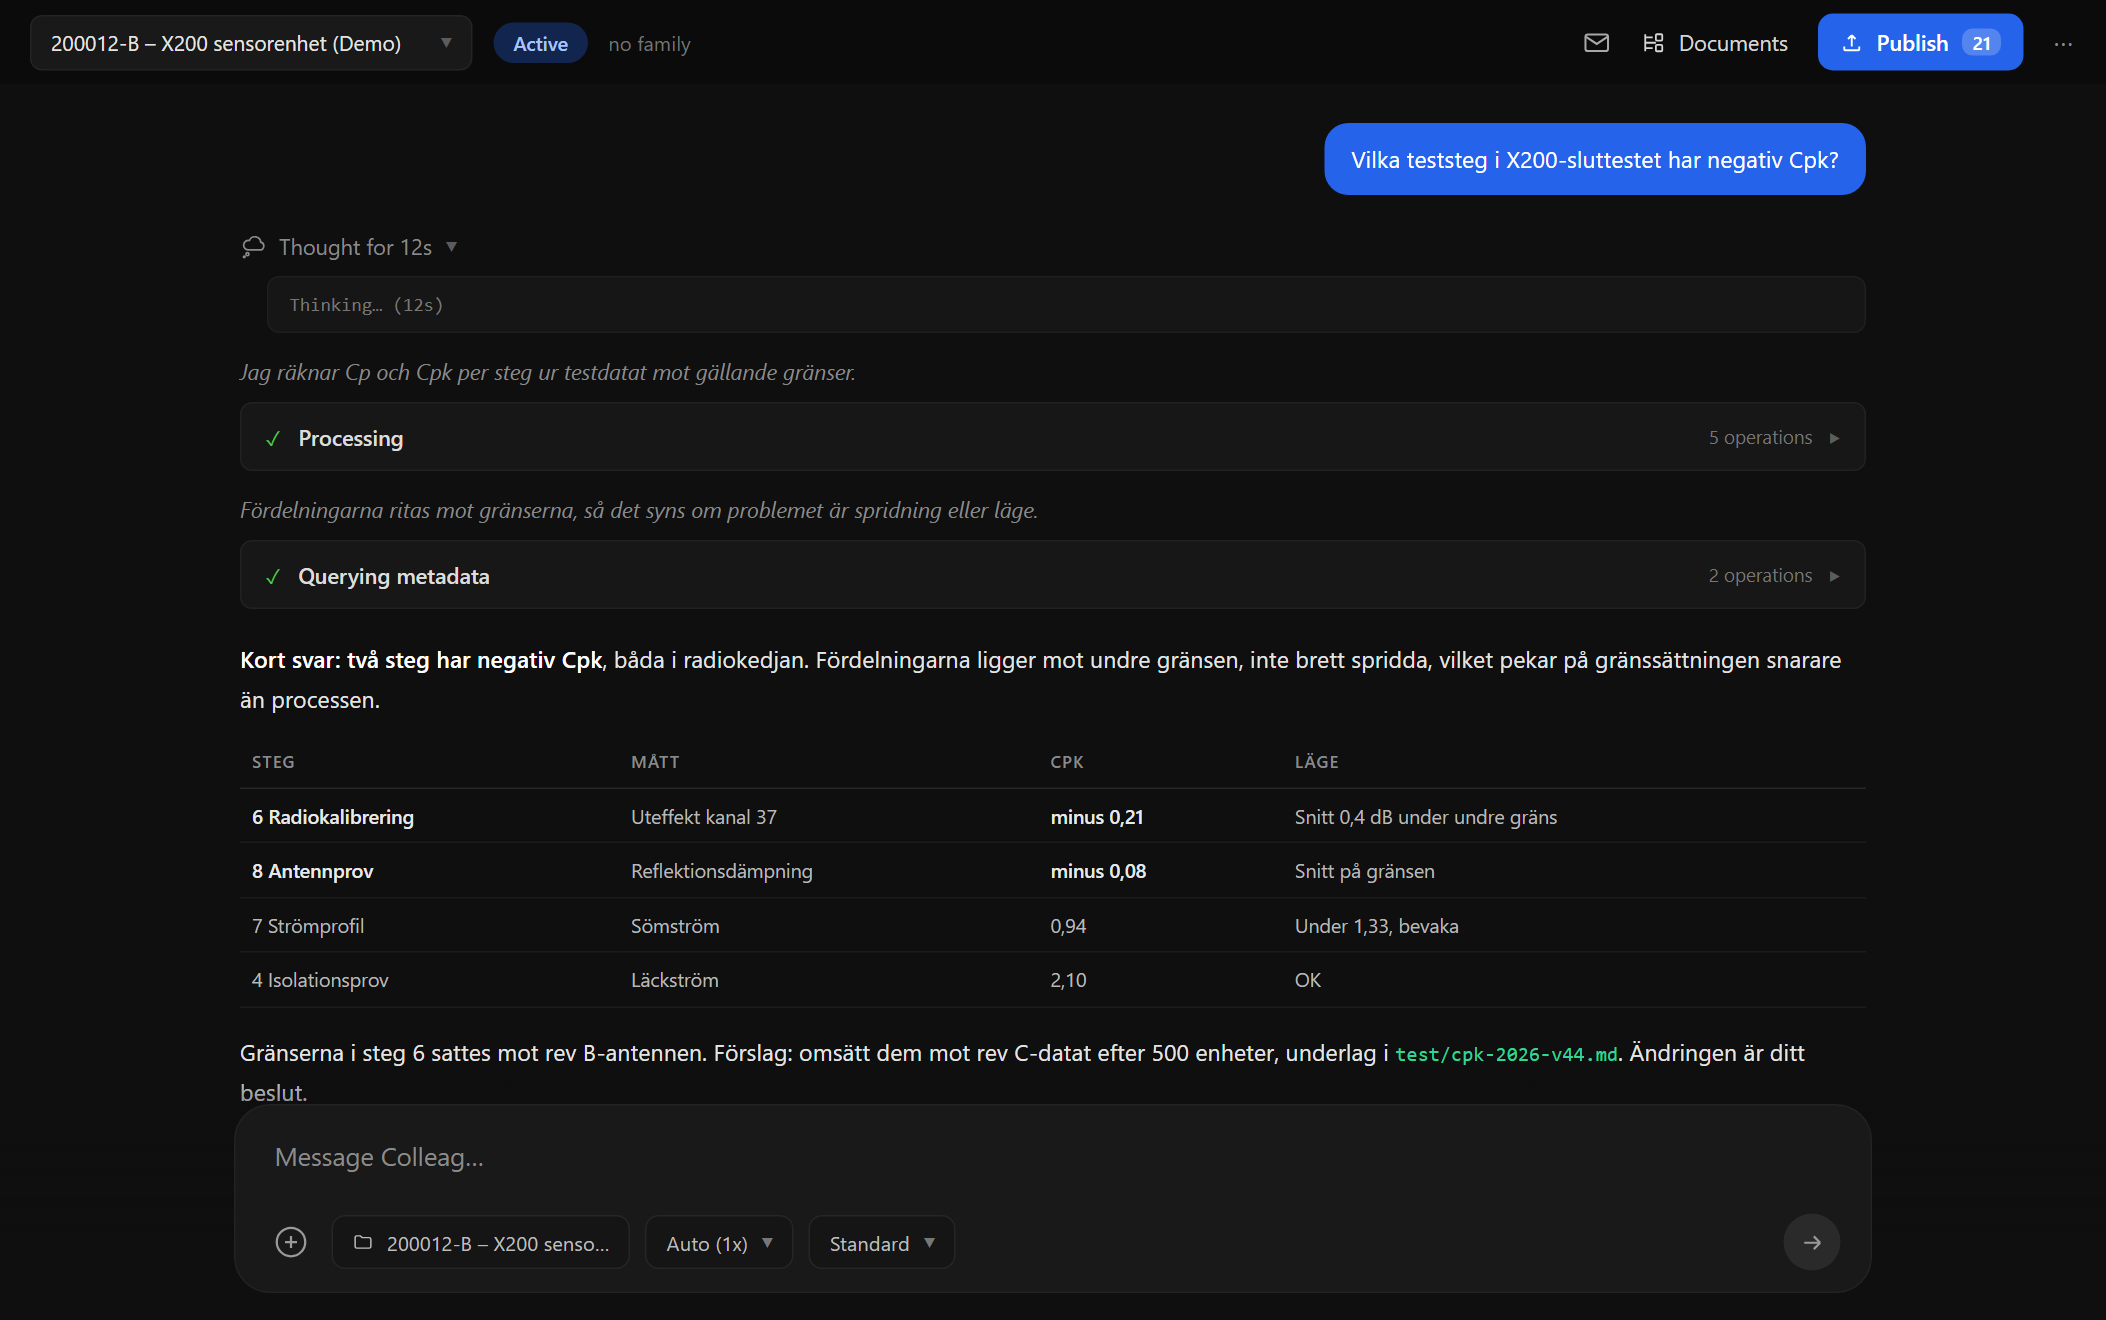
Screenshot from Colleag. The example uses invented figures.
The material
- Test data per step
- Current test limits
- The product prioritization
You approve
Everything the colleague produces is a proposal with sources. Nothing is published, sent or saved to the archive without a human approving it, and every figure traces to its material.
Curious what it feels like?
We run pilot programs with a few manufacturing companies at a time. Tell us about your business and we will show what the colleagues can do with your documents and your data.